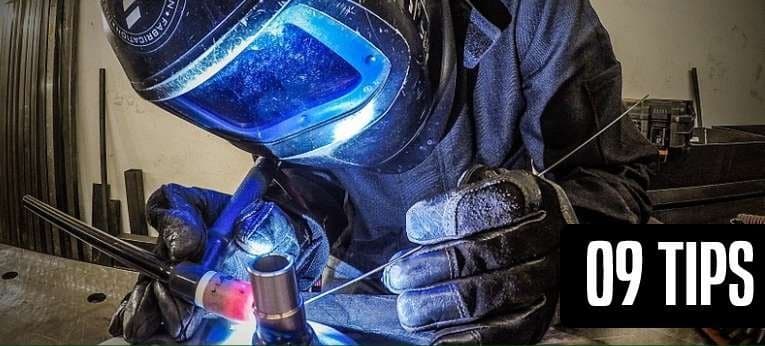
To use a TIG welder: set DC electrode negative for steel and stainless, AC for aluminium. Fit a tungsten sized to the current - 1/16 inch up to about 100 amps, 3/32 inch for general work. Set roughly one amp per thousandth of an inch of steel thickness, argon at 15 to 20 cubic feet per hour, and feed the filler with your other hand.
What TIG is, and why it is slow
The arc runs between a pointed tungsten electrode and the work, under argon. TWI make the point that matters: because the electrode is not consumed, the welder does not have to balance the heat of the arc against metal being deposited from it. Heat and filler are two separate controls - usually a foot pedal and your left hand. That is the whole reason TIG is precise, and the whole reason it is slow: TWI note the deposition rate is low, and recommend stick or MIG for heavy sections. MIG against TIG covers the trade in full.
Setting the machine: polarity, then amperage, then gas
Polarity first, because it is the setting that is either right or useless. TWI explain that arc heat divides roughly one third at the negative pole and two thirds at the positive, so in DC the electrode is kept negative to stop it overheating and melting. Aluminium is the exception: on AC the workpiece spends part of each cycle as the cathode and, in TWI's words, the surface is cleaned of oxide contamination.
What to set, and why
| Setting | Steel and stainless | Aluminium |
|---|---|---|
| Polarity | DC electrode negative | AC |
| Why | Keeps the tungsten cool; two thirds of the heat goes into the work | Part of each cycle strips the oxide skin, which DC cannot do |
| Tungsten | Ground to a point, marks lengthwise | Rounded tip; it will ball itself in the arc |
| Starting amperage | About 1 amp per 0.001 inch of thickness | More - aluminium carries heat away faster |
So 1/8 inch steel is 0.125 inch, which is about 125 amps to start from. The pedal is there so you can be wrong and correct it mid-bead; the dial sets the ceiling.
Gas last. CK Worldwide give 15 to 20 cubic feet per hour as typical, and say to increase it slightly for a larger cup or a gas lens. More is not better - too much flow becomes turbulent and pulls air into the shield, which is the opposite of what you wanted. TIG runs on pure argon rather than a mix, because tungsten is attacked by oxygen and CO2; which gas for which job goes through the rest.
Tungsten: size it, choose it, and grind it properly
Tungsten diameter against current, per CK Worldwide
| Diameter | Use |
|---|---|
| 1/16 inch (1.6 mm) | Light work, up to about 100 amps |
| 3/32 inch (2.4 mm) | The general-purpose size, and what most work uses |
| 1/8 inch (3.2 mm) | High amperage or thick material |
Type matters less than people think, with one exception. Two percent lanthanated, the blue one, runs on AC and DC and is the single electrode to own if you own one. The red thoriated is the one to stop buying: thorium is radioactive and grinding a point makes a dust of it - the full colour chart is in types of welding rods.
AC settings, for aluminium
Two controls, and both of them are misread constantly. AC balance sets how much of each cycle cleans oxide off against how much melts metal. The trap is that machines do not count it the same way: some publish it as percent electrode positive, some as percent electrode negative, and the same number means opposite things - our comparison of TIG machines shows three manufacturers doing it three ways. Read your own manual before copying a setting off the internet.
Frank Armao, who chairs the AWS D1 Aluminum Subcommittee, recommends running balance as low on the electrode-positive side as will still clean the metal: about 35% EP on older transformer machines, and as little as 15% on a modern inverter.
AC frequency is the other one. CK Worldwide describe the effect plainly: a higher frequency, 100 to 250 Hz, gives a narrow focused arc for precision work, while a lower one around 60 Hz gives a wider arc and more cleaning action. Thin aluminium usually wants the wider arc.
Safety, and the shade number for TIG
TIG amperages are lower than stick, so the shade is often set too dark to see the puddle or too light to be safe. OSHA publish the bands for gas tungsten arc welding specifically, and they are not the same as the stick ones.
Filter shade for TIG (GTAW)
| Arc current | OSHA minimum | ANSI and AWS suggested |
|---|---|---|
| Under 50 A | 8 | 10 |
| 50-150 A | 8 | 12 |
| More than 150-500 A | 10 | 14 |
Below that, the usual rules apply and one of them is specific to TIG: the arc is small, concentrated and held close to your hands, so bare forearms get burnt in minutes. TIG gloves are deliberately thin so you can feel the rod, which means they protect less - what a flame-resistant shirt actually certifies matters more here than on any other process.
Welding: the sequence
- Clean the joint to bright metal, and degrease it. TIG is the least tolerant process there is of oil, paint and oxide
- Fit the tungsten with about one electrode diameter of stick-out from the cup for a butt joint; more for a fillet, where you need to reach into the corner
- Set polarity, then amperage, then gas flow. Check the polarity rather than assuming it
- Start the gas flowing and let the post-flow setting be long enough to shield the tungsten while it cools - a tungsten that oxidises as it cools is contaminated for the next weld
- Strike with high frequency or lift-arc, holding the tungsten a rod-diameter off the plate. It should never touch
- Build a puddle before you add anything. The filler goes in when the metal is molten and not before
- Dip the filler into the leading edge of the puddle, not into the arc, and withdraw it without leaving the gas shield
- Move the torch forward a puddle-width and repeat. The rhythm is dip, move, dip, move
- Taper the pedal off at the end rather than lifting straight off, so the crater fills instead of cracking
Reading the weld: what went wrong
TIG faults
| What you see | Why | Fix |
|---|---|---|
| The tungsten touches and the arc goes out | Arc held too close, or unsteady hand | Stop. Regrind or replace the tungsten - a dipped electrode contaminates every weld after it |
| Black soot around the bead | Not enough gas, or too much and turbulent, or a leak | Check the flow is 15-20 CFH, then check the hose and the back cap |
| The weld is porous | Dirty or oily metal, or air pulled into the shield | Clean to bright metal and degrease; check for a draught |
| Grey or crusty stainless underneath | Sugaring - the back of the joint oxidised | Back-purge the joint with argon, or accept it will not be a code weld |
| The arc wanders | Tungsten ground across instead of lengthwise, or contaminated | Regrind lengthwise on a wheel kept for tungsten |
| Aluminium goes dull and will not wet out | Oxide not being cleaned - balance too far to electrode negative | Move balance toward electrode positive, and check which way your machine counts |
Frequently asked questions
What amperage should I use for TIG welding?
About one amp per thousandth of an inch of steel thickness as a starting point, so around 125 amps for 1/8 inch. Aluminium needs more because it carries heat away faster. The older advice on this page - 250 amps - was wrong for almost all work, and would destroy a 1/16 inch tungsten, which CK Worldwide rate to about 100 amps.
Which tungsten should I buy?
Two percent lanthanated, the blue one, in 3/32 inch. It works on both AC and DC, which no other common type does well, and it is not radioactive. Add 1/16 inch for thin work. Avoid the red thoriated: it contains thorium oxide, and you grind these constantly.
How much gas flow does TIG need?
15 to 20 cubic feet per hour is the usual range, a little more for a large cup or a gas lens. Turning it up further makes the flow turbulent and pulls air into the shield, which produces exactly the porosity you were trying to avoid.
Why does my tungsten keep contaminating?
It is touching the puddle or the filler rod. The tungsten should never make contact - hold it about a rod-diameter off the plate and dip the filler into the leading edge of the puddle rather than into the arc. Once it has touched, stop and regrind; a contaminated tungsten spoils everything welded after it.
Do I need AC to weld aluminium with TIG?
Yes. Aluminium carries a surface oxide that melts far hotter than the metal beneath it, and only the electrode-positive half of an AC cycle strips it. A DC-only TIG machine welds steel and stainless well and will not weld aluminium at all.
Sources
- TWI - Tungsten inert gas (TIG/GTA) welding: the non-consumable electrode, polarity, and why aluminium needs AC
- CK Worldwide - guide to AC/DC TIG welding: tungsten sizing, gas flow, grinding direction, AC frequency
- OSHA - Eye protection against radiant energy during welding: the GTAW shade bands (PDF)
- Frank Armao, chair of the AWS D1 Aluminum Subcommittee - setting AC balance for aluminium GTAW
- ANSI/AWS Z49.1:2021, Safety in Welding, Cutting and Allied Processes (free PDF)
In short
Polarity decides whether the machine can do the job at all, amperage decides whether the bead is any good, and the tungsten decides whether the arc is stable - in that order. Start at about one amp per thousandth of an inch, argon at 15 to 20 CFH, a 3/32 inch lanthanated tungsten ground lengthwise, and a shade that lets you see the puddle. Everything after that is the rhythm of dip, move, dip, move, and that part only comes from hours.